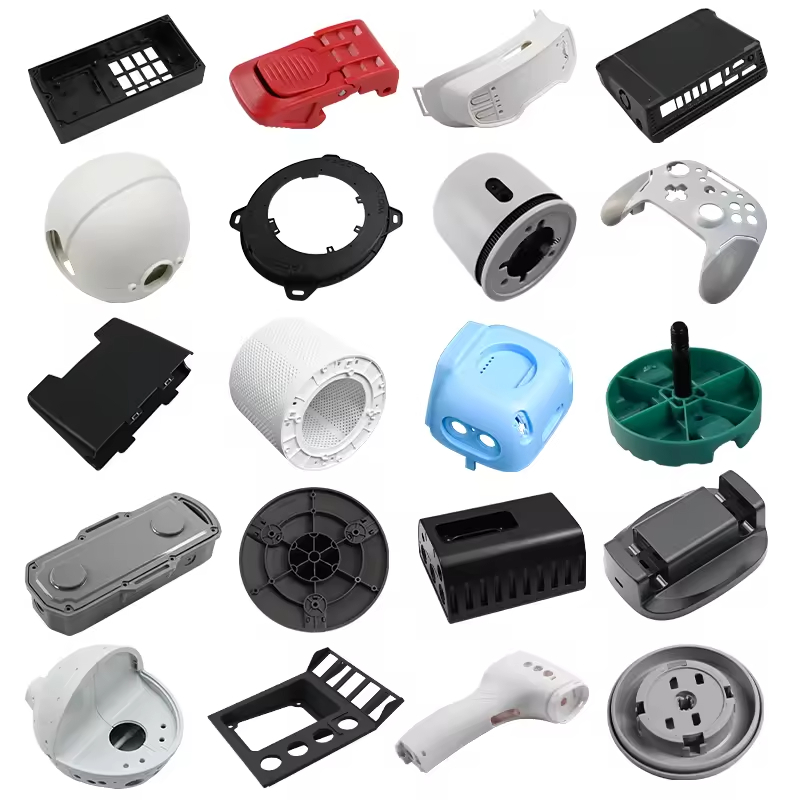
Choosing a plastic enclosure manufacturer starts with the operating environment, PCB and connector envelope, sealing requirement, assembly method, and expected demand. The right supplier should connect material selection, tooling, molding, inserts, finishing, inspection, and assembly instead of treating the enclosure shells as an isolated quote.
A housing that looks simple can still fail through warpage, poor gasket compression, cracked bosses, connector misalignment, inadequate heat paths, or cosmetic variation. Define those risks before tooling so the supplier can recommend a controlled manufacturing route.
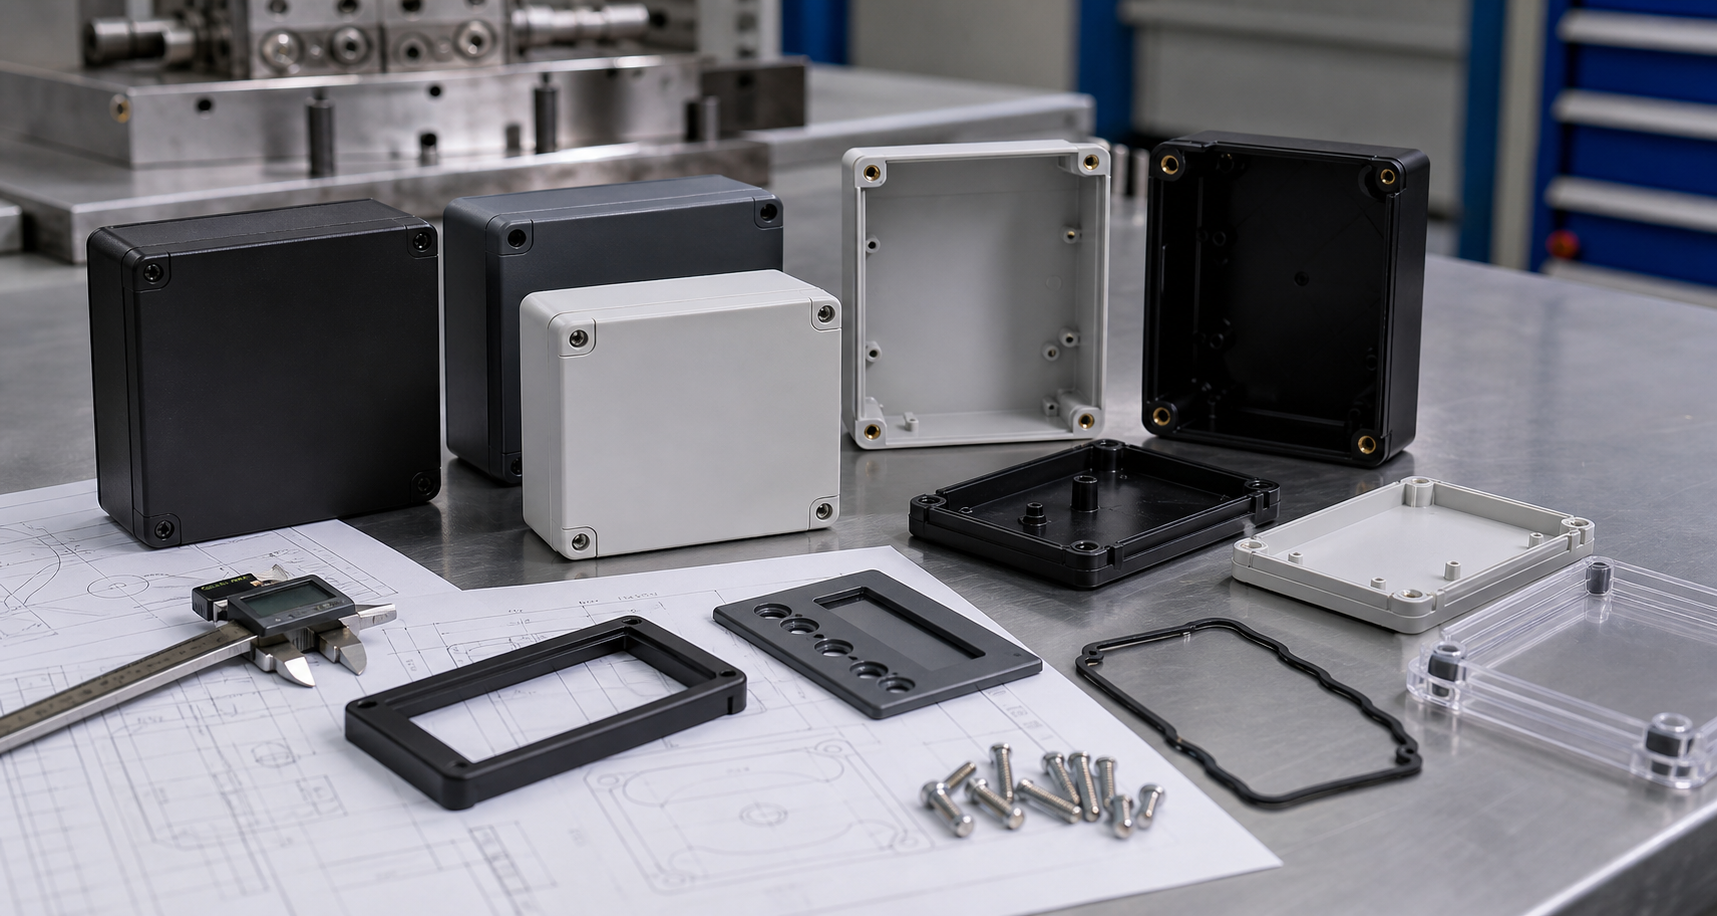
What a Plastic Enclosure Supplier Should Control
| Decision area | Why it matters | What to confirm before quoting |
|---|---|---|
| 재료 | Controls impact, heat, UV, flame, chemical and electrical behavior | Resin grade, thickness, environment, color and required tests |
| 벽 및 리브 설계 | Affects sink, warpage, stiffness and cosmetic consistency | DFM review, nominal wall, rib ratio, draft and gate strategy |
| Joint and seal | Determines ingress protection, assembly force and serviceability | Gasket, weld, adhesive or snap-fit method and compression range |
| PCB and connector fit | Small position errors can prevent installation or cable engagement | Controlled datums, connector keep-outs, bosses and tolerance stack |
| Assembly scope | Shell price alone may not represent the finished product cost | Inserts, printing, labels, shielding, gasket and final inspection |
Map the Enclosure Requirements First
Before selecting a polymer, document whether the enclosure is indoor, outdoor, exposed to cleaning chemicals, near a heat source, or installed where impact and vibration matter. Record the PCB envelope, connector locations, cable bend radius, fastener access, service openings, cosmetic zones, target ingress protection, and annual volume.
For electronics, also define flame, electrical spacing, CTI, ESD, EMI shielding, grounding, and thermal requirements. These are product-level requirements, not automatic properties of a polymer family. A specific grade, wall thickness, construction and test method must support the claim.
Material Selection for Heat, Flame, UV, Impact and ESD
| 요구 사항 | Possible material direction | Risk to validate |
|---|---|---|
| General indoor housing | ABS or PC/ABS | Impact, heat, finish, flame grade and stress cracking |
| High impact or transparent window | PC or a qualified PC blend | UV exposure, chemical cleaning, mold release and optical quality |
| Electrical or dimensional stability | PBT or reinforced PA | Moisture, warpage, CTI, connector fit and flow direction |
| 야외 노출 | UV-stabilized grade or protected finish | Color shift, embrittlement, seal aging and temperature cycling |
| ESD or conductive need | Qualified dissipative compound, conductive compound or coating | Resistance range, appearance, grounding and shielding continuity |
Use the selected grade’s datasheet and customer requirements to define testing. UL94, CTI, ESD and outdoor durability cannot be promised from the material name alone. Moisture-sensitive materials also need a controlled drying and conditioning plan before molding and inspection.
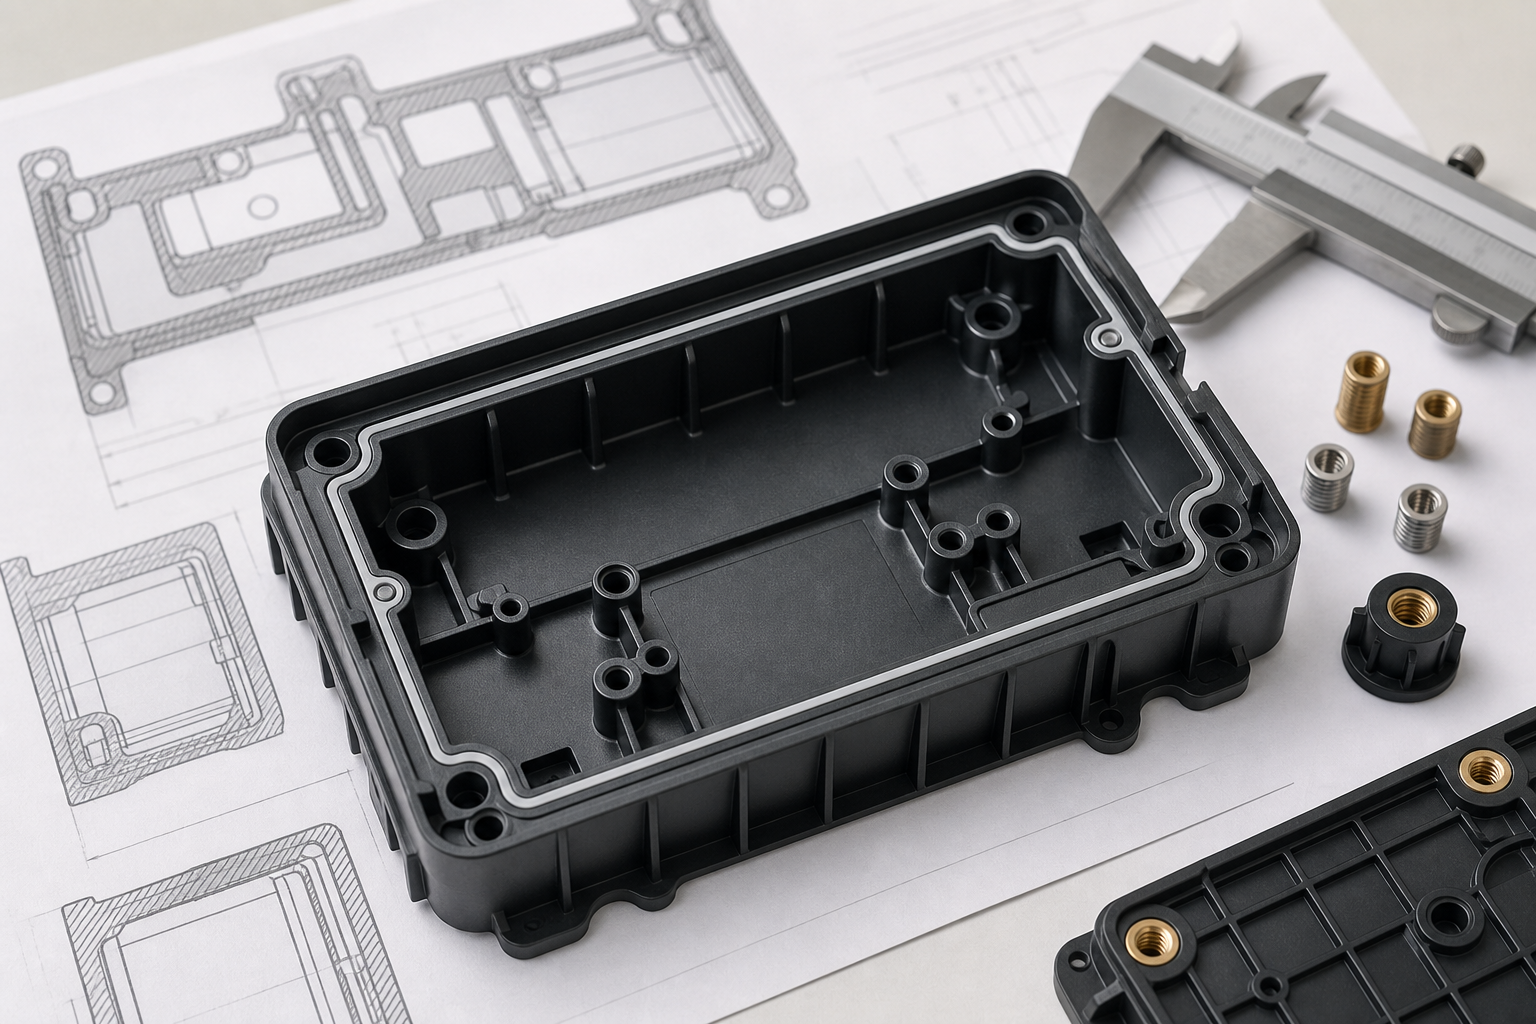
Molding, CNC or Additive Manufacturing?
Injection molding is usually the best route when the enclosure design is stable, the expected volume justifies tooling, and the program needs repeatable texture, integrated bosses, consistent sealing surfaces, and predictable assembly cost. CNC machining is useful for early validation, low quantities, machined openings, and designs that are still changing. Additive manufacturing can support form-and-fit studies and pilot builds, but its surface, anisotropy, sealing behavior and material certification may differ from molded parts.
| Project condition | Likely route | Buyer should verify |
|---|---|---|
| Stable design and repeat volume | 사출 성형 | Tool life, cavity plan, cycle time, cooling and production inspection |
| Low quantity or frequent revisions | CNC 가공 | Material stock, assembly fit, machining access and surface finish |
| Fast form-and-fit iteration | Additive manufacturing | Orientation, surface, clearance, post-processing and material limits |
| Launch before final tool completion | Rapid or bridge tooling | Representative resin behavior, tool life, quality limits and transition plan |
Wall, Rib, Boss, Vent and Snap-Fit DFM
Keep nominal walls as consistent as the function allows, core out thick intersections, and use ribs to add stiffness without creating sink or visible read-through. Bosses need enough support for the required screw or insert torque while remaining separated from cosmetic walls. Add draft based on draw depth, resin shrinkage, texture and surface finish rather than using one universal value.
Snap fits should be checked for beam strain, assembly force, retention, repeated cycling and the selected resin’s temperature and moisture condition. Vent openings must balance airflow, dust, liquid exposure, finger access and internal heat paths. Gate position, ejector locations, parting line, weld lines and connector keep-outs should be reviewed before steel release.
Sealing, Inserts, EMI and Secondary Operations
A gasket land needs continuous geometry, controlled flatness, sufficient width, corner treatment and a defined compression range across the complete tolerance stack. An ingress target is a product validation objective, not a molding guarantee. Test the assembled enclosure with production-intent gasket, fasteners, inserts and cable interfaces.
Heat-set, ultrasonic or molded-in inserts should be selected from torque, pull-out load, wall thickness, installation equipment and repairability. EMI solutions may include conductive compounds, coatings, metal shields or grounded inserts. Each option needs a continuity, grounding, corrosion and assembly inspection strategy. Labels, laser marks, printing, painting, ultrasonic welding and adhesive bonding should be validated on the production resin and texture.

Common Enclosure Risks and Practical Controls
| 위험 | Typical cause | Control before production approval |
|---|---|---|
| 뒤틀린 하우징 반쪽들 | Uneven walls, fiber orientation, unbalanced cooling or packing | DFM thickness review, flow/cooling review, free-state inspection and assembly trial |
| 누출 또는 개스킷 압착 불량 | Seal path, flatness or tolerance stack not defined together | Compression study, fixture condition, leak test and production-intent gasket |
| Cracked bosses or loose inserts | Fastening load exceeds the local plastic design | Torque/pull-out test, boss review, insert specification and repair plan |
| Connector or PCB misalignment | Datums, boss position and shell variation accumulate | Assembly fixture, connector engagement test and cavity-specific dimensional data |
| 화장품 거부 반응 | Material, texture, weld line or viewing standard chosen too late | Approved limit samples, controlled lighting and defined cosmetic zones |
Inspection and Assembly Validation
Inspect PCB and connector datums, gasket lands, split-line mismatch, boss position, insert height, overall warpage and cosmetic zones. Functional checks may include screw torque, insert pull-out, snap cycling, leak testing, thermal exposure, drop, vibration, shielding continuity or electrical spacing, depending on the application.
Use production-intent components for validation. A housing can meet individual drawing dimensions and still fail at system level when a connector, gasket, fastener, PCB or cable is introduced. The inspection record should identify drawing revision, resin grade and lot, cavity, fixture condition, instrument, sample quantity, actual result and disposition.
Supplier Qualification and Project Handoff
Before awarding the tool, ask how the supplier separates design review, mold design, trial molding, inspection, assembly and production release. A clear handoff prevents the tooling team from losing information about the PCB, gasket, connector, cosmetic zones or customer test requirements.
| Qualification question | Evidence to request | Why it matters |
|---|---|---|
| Can the supplier control the full enclosure path? | DFM review, mold plan, molding, secondary operations and assembly scope | Reduces gaps between shell production and finished-unit acceptance |
| How are critical features tracked? | Ballooned drawing, datum plan, cavity identification and dimensional report | Connects the drawing requirement to measurable production evidence |
| How are material and process changes handled? | Change notice, affected-feature review, sample approval and revised records | Protects fit, flame, ESD, sealing and cosmetic performance after release |
| How is assembly validated? | Production-intent PCB, connector, gasket, fasteners and functional test record | Finds system-level failures that shell-only inspection cannot show |
Change Control and Production Continuity
Enclosures often remain in production long enough to experience resin substitutions, electronic revisions, tool maintenance, supplier changes, or a move between molding cells. Define which changes require customer approval before production resumes. A replacement resin, colorant, gasket, insert or tool component can affect dimensions, flame behavior, sealing, conductivity, surface appearance or assembly force.
Maintain the approved drawing revision, material grade, mold identification, cavity records, inspection method, limit samples and assembly test method together. When a change is proposed, identify the affected characteristics, repeat the relevant dimensional or functional tests, and retain the approval record with the new revision. This is especially important for sealed, flame-rated, ESD-sensitive or connector-heavy housings. Ask the supplier to identify a backup plan for resin supply, tool maintenance and replacement parts.
Custom Enclosure RFQ Checklist
- 3D CAD, controlled drawings, PCB and connector envelope, and revision level.
- Environment, thermal load, resin or standard requirements, and target ingress rating.
- Annual demand, program life, color, texture, cosmetic zones and approval samples.
- Insert, fastener, gasket, label, shielding, welding and final assembly scope.
- Critical datums, tolerance stack, connector engagement, seal test and inspection method.
- Required reports, material records, cavity traceability, functional tests and packaging.
Send the CAD assembly, environment, finish, sealing target and annual volume with the RFQ. We can review the material, tooling, assembly and inspection path before quoting the production route.
Enclosure Decisions That Should Be Closed Before Tooling
| 요구 사항 | Typical Failure If It Is Vague | RFQ Evidence |
|---|---|---|
| Sealing and environment | Gasket compression, screw bosses, vents, or joint flatness do not support the intended exposure | IP target, fluid, pressure, temperature, gasket, and test method |
| PCB and connector envelope | Warpage or draft interferes with assembly and cable or connector alignment | Controlled assembly, keep-outs, datum scheme, and mating parts |
| Heat, flame or ESD | Material selected from appearance or price cannot meet the electrical or thermal requirement | Temperature, UL or other requirement, ESD target, and exact grade |
| Quantity and change rate | Tooling route is chosen before the design and annual demand are stable | Prototype, pilot, annual volume, revision plan, and ownership terms |
How Nylon Plastic Supports the Project
Nylon Plastic has supported material selection and finished plastic-part manufacturing since 2005. For custom plastic enclosures, the useful review connects the drawing, material, tooling or machining route, inspection state, and production plan before a quote is approved.
- Connect unfilled PA, PA-GF20, PA-CF30, PC, ABS, and other candidates to heat, impact, flame, ESD, UV, moisture, and appearance needs.
- Review molding, CNC machining, 3D printing, inserts, sealing, finishing, assembly, and inspection as one project instead of isolated line items.
- Define critical datums, gasket and connector interfaces, material documentation, sample approval, packaging, and change control before volume release.
관련 읽기
자주 묻는 질문
How do I choose a plastic enclosure manufacturer?
Compare material and environmental capability, DFM, tooling, sealing, inserts, assembly, inspection, change control, communication, and the supplier’s ability to hold the same acceptance standard over repeat orders.
Should a plastic enclosure be molded, machined, or 3D printed?
Use molding when the design is stable and volume supports tooling, CNC for low-volume or tight stock-form features, and 3D printing for rapid iteration or complex low-volume parts after process limits are accepted.
What material is best for a custom enclosure?
There is no universal best material. Compare heat, impact, flame, ESD, UV, chemical exposure, moisture, finish, wall design, and approval requirements against the exact grade.
What should be sent for an enclosure manufacturing quote?
Send the CAD assembly, controlled drawing, quantity by phase, environment, finish, PCB and connector details, insert and seal requirements, assembly scope, inspection, and packaging needs.
Request a Custom Enclosure Manufacturing Review
Send the enclosure assembly, requirements, quantity, and critical interfaces for a DFM, material, tooling, and production-route review.