Melt temperature versus mold temperature is a common source of confusion in injection molding. Melt temperature controls the viscosity, flow behavior, thermal history and degradation risk of the resin as it enters the cavity. Mold temperature controls the thermal boundary at the cavity surface, the rate at which the skin freezes, surface replication, crystallization for semi-crystalline grades, cooling balance and the dimensions reached after ejection.
They are related but not interchangeable. Raising melt temperature may reduce fill resistance, but it can increase residence-time damage, gas, flash or color change. Raising mold temperature may improve surface finish and weld-line strength, but it can extend the cycle and change shrinkage, crystallinity or warpage. A sound validation record uses measured melt and mold-surface temperatures, not only controller setpoints.
The direct difference
| 온도 | Main function | Part response | Risk when excessive |
|---|---|---|---|
| Melt temperature | Controls viscosity, filling resistance, shear response and material thermal history | Fill pressure, flow-front stability, weld-line formation, degradation and color | Degradation, gas, splay, discoloration, flash or long residence-time exposure |
| Mold-surface temperature | Controls skin freezing, surface replication, cooling and crystallization | Gloss, texture, weld-line strength, shrinkage, flatness and ejection | Long cycle, sticking, flash, dimensional movement or thermal imbalance |
| Coolant in/out temperature | Controls heat removal through each circuit | Cavity balance, hot spots, cycle repeatability and warpage | Scale, blocked channels, leakage or an inaccurate controller reading |
다음의 process window and setup-sheet guide for how temperature values fit into a complete molding record. The nylon processing guide covers drying and grade-specific limits. The defect guide helps separate a temperature issue from venting, gate, material or geometry causes.
Measuring actual melt temperature
Barrel setpoints are not the same as melt temperature. The material may be heated by the barrel, shear, residence time and back pressure, while heat is lost at the nozzle and during sampling. A temperature probe or documented sampling method should be used when the resin has a narrow processing range, is moisture-sensitive, is filled, or is showing signs of degradation. Record the location, sampling condition, screw recovery state and any delay before measurement.
Compare actual melt temperature with the resin supplier’s recommended range and the material’s visible response. Unusually high pressure at a normal fill time may indicate a cold melt, a frozen gate or a restriction. A low pressure trace with burn marks, odor, dark specks or color drift may indicate excessive thermal history rather than a healthy process. Temperature should be judged together with fill time, screw recovery, back pressure, residence time and material lot.
Mold-surface temperature and thermal balance
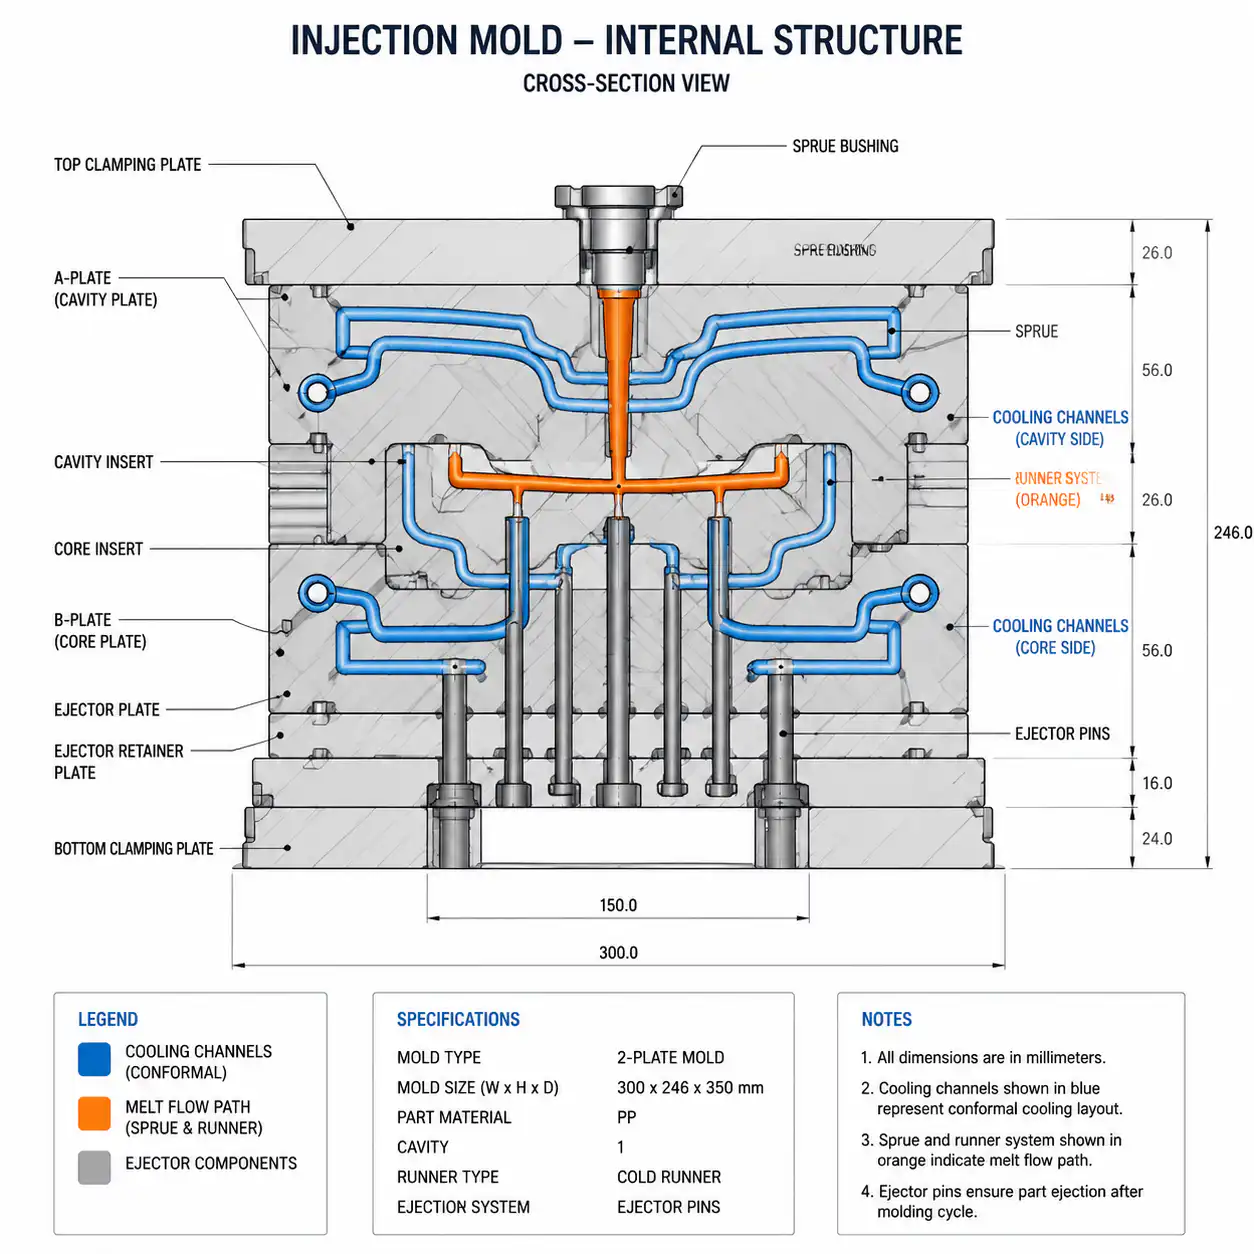
The mold controller may display the temperature of the supply or return line, while the part responds to the surface temperature at the cavity and core. Measure the surface near the gate, the thickest section, the cosmetic face and the areas associated with warpage or gloss variation. Record coolant inlet/outlet temperatures, flow if available, circuit identification and the time allowed for the mold to reach thermal balance.
Unequal circuits can create a part that looks acceptable at one point in the cycle and moves after ejection or conditioning. A blocked channel, baffle, bubbler, insert or scale buildup can change the local heat-transfer response. For multi-cavity tools, compare cavity-specific surface temperatures and dimensions. A stable controller display does not prove that all cavities see the same thermal condition.
Amorphous versus semi-crystalline resin response
Amorphous materials such as ABS and PC do not form a crystalline structure during cooling, so mold temperature mainly affects viscosity at the surface, skin freezing, replication, residual stress and dimensional relaxation. A warmer mold may improve weld-line strength and surface appearance, but it can also increase cycle time and make ejection more demanding.
Semi-crystalline materials such as PA, POM, PP and PEEK develop crystallinity as they cool. Mold temperature influences the rate and degree of crystallization, which affects shrinkage, stiffness, chemical resistance, surface appearance and post-molding dimensions. The same melt temperature can produce a different result when mold temperature or cooling time changes. For reinforced grades, fiber orientation can add directional shrinkage on top of the resin’s thermal response.
| Resin response | Melt-temperature influence | Mold-temperature influence | Inspection focus |
|---|---|---|---|
| Amorphous resin | Viscosity, fill pressure, shear and degradation | Surface replication, stress, weld lines and relaxation | Appearance, dimensions after conditioning and stress cracking |
| 반결정성 수지 | Flow, thermal history and degradation | Crystallization, shrinkage, stiffness and cooling balance | Dimensions after defined conditioning, flatness and function |
| 유리 섬유 강화 수지 | Viscosity, fiber breakage and orientation during flow | Skin freezing, orientation-related shrinkage and cooling | Flow/transverse dimensions, warpage, gate and weld-line strength |
Effects on fill, weld lines and surface finish
If the melt is too cold for the flow path, the pressure requirement rises and the frozen layer grows earlier. Thin walls, long flow lengths and small gates become more sensitive. A warmer melt can improve flow, but the change should be limited by the resin range, residence time and degradation evidence. A warmer mold can keep the flow front mobile near the surface and improve replication, especially on textured or cosmetic parts.
Weld-line strength depends on the temperature and pressure when fronts meet, the material’s thermal history, the gate and vent design, and the local geometry. Temperature alone cannot repair a poor meeting angle or trapped air. Record the weld-line location, short-shot flow fronts and cosmetic or mechanical requirement before changing the thermal settings.
Effects on shrinkage, crystallinity and warpage
Temperature changes affect more than fill pressure. A higher mold temperature can increase crystallinity in semi-crystalline grades and change final shrinkage. A higher melt temperature can change orientation, relaxation and the cooling history through the wall. Different core and cavity temperatures can create differential shrinkage and warpage. Filled materials may respond directionally because fibers follow the flow path and constrain movement differently in the flow and transverse directions.
Measure the part in a defined condition. For moisture-sensitive nylon, state drying, conditioning temperature, humidity and elapsed time. For a flexible cover, state free-state support and datum alignment. For a sealing or mating part, include assembled measurements at the relevant service condition. A dimensional change after conditioning should not be blamed on mold temperature without checking moisture uptake and material state.
Temperature troubleshooting matrix
| Observed symptom | Temperature evidence | Controlled trial | Other causes to exclude |
|---|---|---|---|
| Short shot or high fill pressure | Measured melt, mold-surface temperature and fill time | Small melt or mold-temperature change within the resin range | Gate restriction, venting, material moisture, wall thickness or machine limit |
| Poor texture or gloss variation | Surface temperature map and circuit balance | Compare surface temperature at cosmetic zones and adjust thermal balance | Texture condition, packing, flow front, mold polish and contamination |
| Weld-line weakness or visible line | Flow-front temperature at meeting zone and mold temperature | Check temperature with gate/vent and fill profile changes | Gate location, air trap, meeting angle and local thickness |
| Warpage or post-mold movement | Core/cavity temperatures, coolant balance and conditioning state | Compare balanced cooling and defined conditioning samples | Packing, fiber orientation, wall map, gate and inspection fixture |
| Burning, dark specks or odor | Actual melt temperature, residence time and recovery condition | Reduce thermal exposure and verify purge/material condition | Trapped gas, contamination, dead spots, shear and venting |
Validation and setup-sheet checklist
- Record resin manufacturer, exact grade, color, reinforcement and lot.
- Record dryer temperature, time, dew point or moisture reading where relevant.
- Record barrel setpoints, measured melt temperature and sampling method.
- Record mold controller setpoint, core/cavity surface temperatures, coolant inlet/outlet and circuit identity.
- Record fill time, speed profile, transfer, packing, cooling, recovery and cycle.
- Inspect appearance, weld lines, texture, dimensions, flatness, weight and ejection.
- Condition moisture-sensitive parts before final dimensional acceptance.
- Approve the center condition and permitted range using consecutive shots from every cavity.
For an RFQ or troubleshooting review, send the resin and grade, drying record, barrel profile, measured melt temperature, mold-temperature readings, cooling circuit map, cycle, defect photos, controlled drawing and annual volume. We can then separate a temperature correction from a gate, venting, packing, cooling or DFM correction and define the evidence needed before a process window is approved.
The melt temperature vs mold temperature relationship should be validated separately because the two settings affect flow, skin freeze, crystallinity and shrinkage in different ways.
자주 묻는 질문
배럴 온도는 용융 온도와 같은가요?
아닙니다. 배럴 값은 히터 구역의 설정값입니다. 실제 용융 온도는 전단력, 체류 시간, 배압, 스크류 회수율, 원료 상태 및 열 손실의 영향을 받습니다. 수지나 결함의 특성으로 인해 필요한 경우, 문서화된 측정 방법을 사용하십시오.
왜 핫 몰드를 사용해야 할까요?
금형 온도를 높이면 표면 재현성, 용접선 품질 및 유동 전선의 안정성을 향상시킬 수 있으며, 반결정성 수지의 결정화 과정에도 영향을 미칠 수 있습니다. 이에 따른 장단점으로는 사이클 시간, 이젝션, 수축 및 열 균형 등이 있습니다.
높은 용융 온도로 쇼트 샷을 해결할 수 있을까요?
It can reduce viscosity within the resin supplier’s range, but a short shot may instead come from a gate restriction, venting, moisture, wall thickness or machine limitation. Confirm evidence before increasing thermal exposure.
금형 온도는 수축에 어떤 영향을 미치나요?
이는 성형품의 냉각, 결정화 및 응력 상태를 변화시킵니다. 결과는 수지, 벽 두께, 게이트, 냉각 균형, 성형 압력 및 컨디셔닝에 따라 달라지므로, 정해진 검사 조건에서 치수를 측정해야 합니다.
온도는 어떻게 측정해야 할까요?
방법, 위치 및 상태를 기록하십시오. 적절한 경우 실제 용융량을 측정하고, 중요 구역 근처의 금형 표면을 측정하며, 컨트롤러 디스플레이에만 의존하지 말고 냉각수 유입구/유출구 및 회로 식별 정보를 기록하십시오.