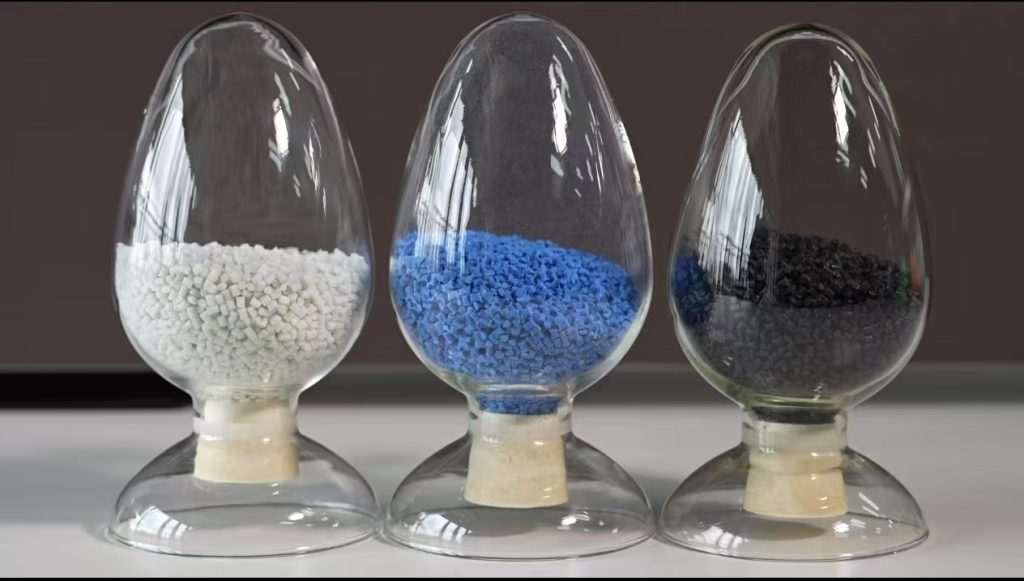
Nylon material selection for injection molding starts with the service condition, not the strongest dry data-sheet value. Choose the PA matrix first, then decide whether the part needs unfilled resin, GF20, GF30, CF30, impact modification, heat stabilization, flame performance, wear additives, or another qualified package.
The drawing should define load, temperature, humidity, chemicals, tolerance state, appearance, annual volume, and approvals before the resin is released for tooling.
적합한 나일론을 선택하는 방법: 체계적인 소재 선정 가이드
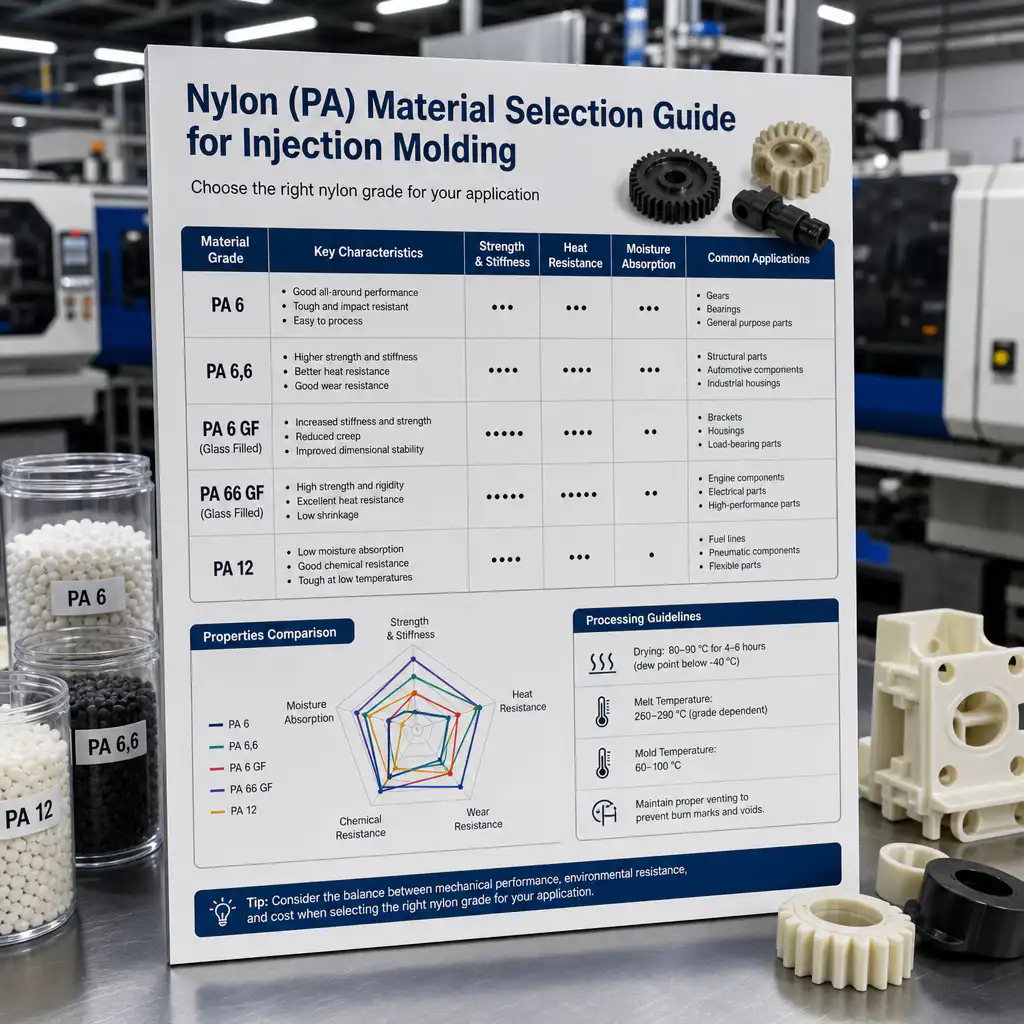
적절한 나일론 등급을 선정하는 것은 엔지니어링 플라스틱 조달 과정에서 가장 중요한 결정 중 하나입니다. 잘못된 선택 — PA6으로도 충분한 곳에 PA66을 선택하거나, 구조용 부품에 충전재가 포함되지 않은 나일론을 지정하는 경우 등 — 은 현장 고장, 생산 지연, 그리고 프로젝트 도중 비용이 많이 드는 자재 교체로 이어질 수 있습니다.
이 가이드에서는 실제 엔지니어링 기준을 바탕으로 한 체계적인 의사결정 프레임워크를 제시합니다: 기계적 요구 사항, 열 환경, 습기 노출, 화학 물질 접촉, 규정 준수 및 비용. 모든 선정 기준은 실제 데이터와 연계되어 있으므로, 일반적인 경험적 지침에 의존하지 않고 증거에 기반한 의사결정을 내릴 수 있습니다.
5가지 핵심 선정 기준
구체적인 등급을 검토하기 전에, 해당 애플리케이션에 대해 이 다섯 가지 기준의 우선순위를 정해 두십시오. 대부분의 애플리케이션이 실패하는 이유는 두 가지 이상의 기준이 상충하기 때문인데, 어떤 기준이 우선시되는지 파악해 두면 나중에 비용이 많이 드는 설계 변경을 피할 수 있습니다.
| 기준 | 그것이 중요한 이유 | 주요 영향 | 2차 영향 |
|---|---|---|---|
| 기계적 강도 | 필요한 하중 지지 능력 | 구조 부품, 브라켓 | 기어 톱니, 베어링 접촉면 |
| 열저항 | 최대 사용 온도 | 엔진 부품, 고온 부위 | 처리 창 |
| 습기 민감성 | 작동 습도 환경 | 치수 안정성 | 전기적 특성 |
| 화학 물질 노출 | 부품과 접촉하는 유체 | 연료, 오일, 산, 알칼리 | 세정제, 용제 |
| 규제 준수 | 시장 및 업계 표준 | 식량, 의약품, 식수 | 자동차, 항공우주 |
PA6 대 PA66: 근본적인 선택
PA6와 PA66은 전 세계 나일론 소비량의 90% 이상을 차지합니다. 이 두 소재의 차이점을 이해하는 것은 모든 소재 선정 결정의 기초가 됩니다.
| 속성 | PA6 | PA66 | 우승자 |
|---|---|---|---|
| 녹는점 | 220~225°C | 260~265°C | PA66 |
| 결정도 | 하단 (~40%) | 상승 (~50%) | 치수 안정성을 위한 PA66 |
| 인장 강도 | 70~85 MPa | 80~90 MPa | PA66 |
| 내충격성 | 더 높은 (더 어려운) | 더 낮음 (더 뻣뻣함) | PA6 |
| 곰팡이 수축 | 1.0-1.5% | 1.3-1.8% | PA6 (뒤틀림이 적음) |
| 수분 흡수 | 8.5-9.0% | 8.0-8.5% | 비슷한 |
| 처리 온도 | 230~260°C | 270~295°C | PA6 (저에너지) |
| 비용 | Lower | 더 높음 | PA6 (20-30%보다 저렴함) |
| 내피로성 | Good | 우수 | PA66 |
강화 등급: 유리 섬유 또는 탄소 섬유를 지정해야 하는 경우
비보강 나일론은 다양한 용도에 잘 활용되지만, 구조용, 고온용 및 고정밀 용도의 경우 거의 항상 보강이 필요합니다. GF30과 GF33(유리섬유)이 주된 소재로 사용되며, 초경량 또는 고강성 용도에는 CF30(탄소섬유)이 선택됩니다.
| 등급 | 인장 강도 | 굴곡 탄성 계수 | HDT (1.82 MPa) | 주요 이점 | 일반적인 애플리케이션 |
|---|---|---|---|---|---|
| PA6 (충진제 미첨가) | 70~85 MPa | 2,800 MPa | 70°C | 견고하고 비용 효율적 | 기어, 부시, 유연한 부품 |
| PA66 (충진제 미첨가) | 80~90 MPa | 3,000 MPa | 80°C | 뻣뻣하고, 내피로성이 뛰어난 | 구조 부품, 베어링 |
| PA6-GF30 | 160~180 MPa | 8,500 MPa | 215°C | 내열성이 뛰어나고 단단함 | 엔진 커버, 브라켓 |
| PA66-GF33 | 190~210 MPa | 10,500 MPa | 250°C | 가장 높은 강성 | 자동차 구조 |
| PA6-GF50 | 200~230 MPa | 15,000 MPa | 220°C | 금속 교체 | 중량용 브라켓 |
| PA66-CF30 | 240~280 MPa | 20,000 MPa | 260°C | 가볍고, 정전기 방전(ESD) 방지 기능이 있음 | 로봇공학, 항공우주 |
| PA12 (충진제 미첨가) | 45~55 MPa | 1,800 MPa | 85°C | 수분 함량이 낮고 유연함 | 유체 시스템, 카테터 |
습도 및 환경: 작동 조건에 맞춘 설정
수분 흡수는 가장 과소평가되는 선정 요인입니다. 엔지니어들은 물이 나일론을 얼마나 극적으로 가소화시켜 탄성 계수를 40%만큼 감소시키고 치수를 상당히 증가시키는지 종종 과소평가합니다.
| 운영 환경 | 권장 학년 | 왜 | 대안 |
|---|---|---|---|
| 건조한 실내 (<50% RH) | PA66 | 치수 정밀도, 강성 | PA6 |
| 습한 실내 (50-80% RH) | PA66-GF30 | 보강 시 습기에 강함 | PA6-GF30 |
| 야외 노출 | PA66-GF30 + UV | 자외선 안정화 처리가 필수적입니다 | PA12 |
| 자동차 엔진룸 | PA66-HT 또는 PA66-GF30 | 150°C 이상에서 열적 안정성이 확보됨 | PA6-GF30 |
| 식수와 접촉 | PA66-GF30 또는 PA12 | NSF/ANSI 61 규격에 부합하는 등급 | PA66 인증 획득 |
| 화학 공장 | PA66 또는 PVDF | 내산·내알칼리성 등급 | PP 또는 HDPE |
| 저온 (-30°C) | PA66 | 저온에서도 강도를 유지합니다 | PA66-GF30 |
| 고온 (>200°C) | PA66-GF30 또는 PPA | PA66 생산 능력 이상 | PEEK 또는 PPS |
After a grade is qualified, the control plan should define how each delivered lot is released. Use the nylon granules incoming inspection guide to connect grade approval with COA review, moisture checks, and traceable material release.
응용 분야별 선택 행렬
단순히 물성만 보고 선택하는 것보다, 재질을 용도 범주에 맞춰 선정해야 올바른 등급을 가장 빠르게 찾을 수 있습니다.
| 신청 부문 | 산업 | 권장 나일론 | 인증 필요 |
|---|---|---|---|
| 공기 흡입 매니폴드 | 자동차 | PA66-GF30 + 열 안정제 | OEM 승인, 엔진룸 내 열 관리 |
| 연료 레일 및 호스 | 자동차 | PA66-GF30 또는 PA12 | EN 594, SAE 배기가스 배출 기준 |
| 전기 커넥터 | E&E, 자동차 | PA66 V-0, PA6 V-2 | UL 94, IEC 60335 |
| 음료용 튜브 및 연결 부품 | 식음료 | PA12, PA66 식품용 | FDA 21 CFR 177.1500, EU 10/2011 |
| 의료기기 하우징 | 의료 | PA66 의료용 등급 | ISO 10993, FDA 510(k) |
| 산업용 기어 및 베어링 | 기계 | PA66-GF30 또는 PA66-CF30 | 필수 항목 없음 |
| 스포츠 용품 | 소비자 | PA6, PA66 | 장난감에 대한 REACH 및 CPSIA |
| 드론 구조 프레임 | 로봇공학/항공 | PA66-CF30 | 전기 제품의 경우 UL 94 V-0 등급 |
Common Buyer Errors Before Tooling Release
| Incomplete Decision | Resulting Risk | Required Check |
|---|---|---|
| Drawing says only nylon | PA6, PA66, PA12, and reinforced grades are quoted as interchangeable | Specify matrix, modification, conditioning, and approval |
| Higher fiber loading is chosen from stiffness alone | Impact, weld line, surface, flow, and tool wear suffer | Compare unfilled PA, GF20, GF30, and CF30 against the failure mode |
| Dry dimensions are used for humid service | Fit and flatness change after conditioning | Define inspection and use-state moisture |
| Grade changes after mold design | Shrinkage, gate, venting, and warpage assumptions become invalid | Approve resin and backup grade before tool release |
나일론 플라스틱이 이 리뷰를 어떻게 뒷받침하는가
Nylon Plastic has worked across material modification and finished plastic-part manufacturing since 2005. This allows buyers to connect the resin decision with mold design, drying, sampling, dimensional validation, and downstream manufacturing rather than approving a grade from a family name or one dry data-sheet value.
- Compare unfilled PA, PA-GF20, and PA-CF30 against the actual failure mode.
- Review custom compounding when a standard grade misses stiffness, impact, color, wear, heat, or compliance requirements.
- Define TDS, COA, moisture, sample approval, traceability, and lot-release requirements before volume ordering.
관련 읽기
자주 묻는 질문
See our PA66 GF33 vs GF40 vs GF60 comparison for detailed grade selection and property data.
Should injection molding material selection start with PA6 or PA66?
Start with the actual heat, moisture, toughness, stiffness, process, cost, and approval requirements. Neither matrix is universally better.
When should PA-GF20 be considered?
GF20 is useful when unfilled PA cannot meet deflection, creep, or shrinkage targets but the project does not need the cost and processing burden of higher reinforcement.
Is PA-CF30 a direct upgrade from glass-filled nylon?
No. CF30 can improve specific stiffness or electrical behavior, but it changes cost, conductivity, anisotropy, brittleness, and processing requirements.
What should be approved before mold production?
Approve the exact grade, backup material, moisture state, shrinkage assumptions, critical dimensions, appearance, compliance, sample plan, and lot documentation.
Request a Nylon Material Selection Review
Send the drawing, annual volume, service environment, current resin, and failure mode for an unfilled PA, GF20, GF30, or CF30 comparison.